TMCO TOOLS
Tooling built by machinists, for machinists.
QUALITY TOOLING, MADE IN-HOUSE
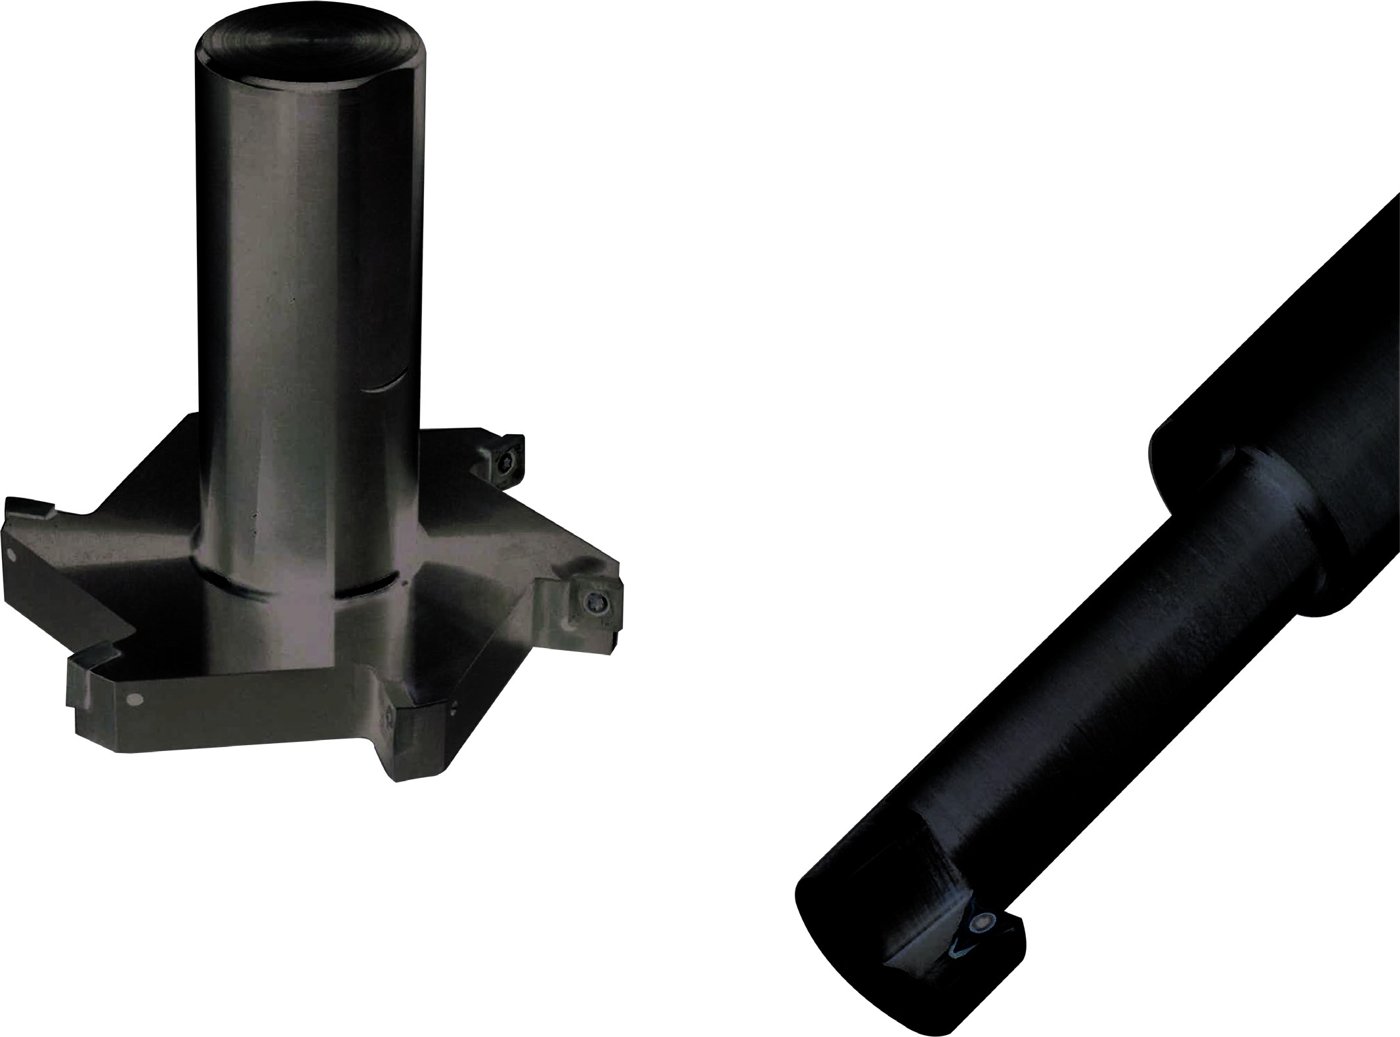
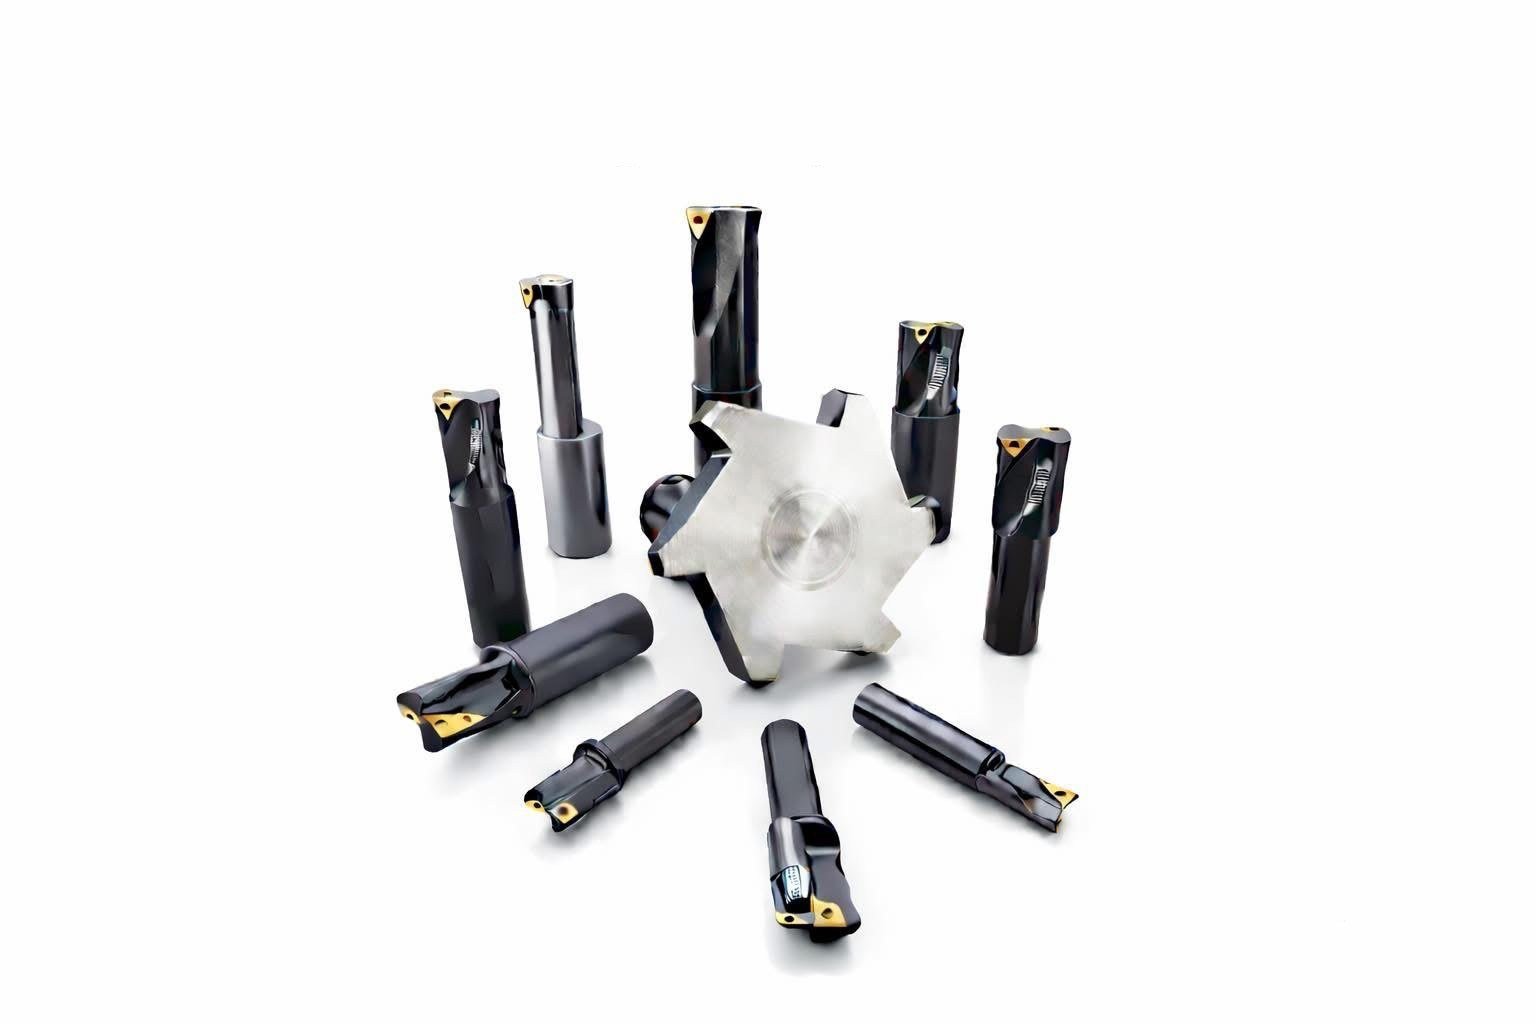
At TMCO Tools, we are committed to developing and manufacturing the highest quality tooling available. Our commitment shows in our product quality, delivery and technical service. TMCO Tools are produced on our double-turret CNC lathes and 4-axis CNC milling centers to create precise tooling at competitive prices.
- Helical flutes for easy chip evacuation
- Strong and free cutting
- Flat bottom, 90° corners
- Coolant-through tooling available
- Easily achieve 63 to micro-finish at suggested speeds & feeds
Specials
TMCO offers a wide range of standard sizes, but some projects demand specially designed tools. Our technical staff will design and produce tools for your unique application.
Safety First
Built for durability, performance and safety. Properly held, applied and maintained, TMCO Tools will serve you well into the future.
Fast Delivery
We keep adequate stock of standard sizes and ship most orders within one day.
Technical Help
Our technical staff is glad to help with any part of your application. Call (814) 432-5281 and we'll help you put our tools to work, fast.
TRY ONE FREE FOR A MONTH
Choose a stock-standard counterbore tool and try it free for a month. If you are not satisfied with its performance, send it back. TMCO Tools pays shipping both ways, no questions asked.
CALL TO START YOUR TRIALINDEXABLE COUNTERBORE TOOLS – INCH
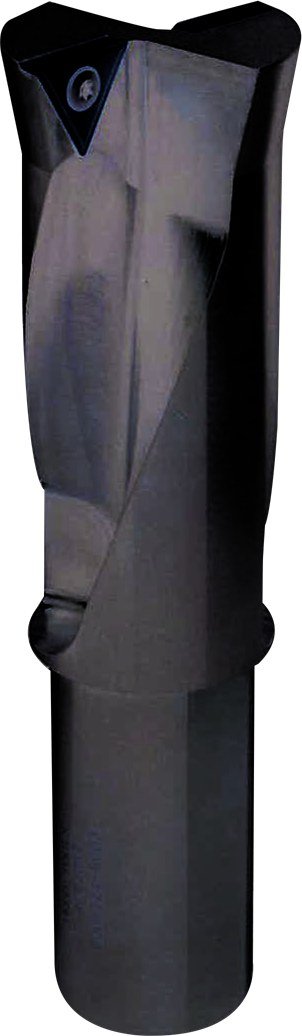
A = cutting diameter · B = shank diameter · L1, L2, L3 = lengths (in.)
| Part No. | A | B | L1 | L2 | L3 | Pre-Drilled Hole | Spare Parts |
|---|---|---|---|---|---|---|---|
| CB0625 | 0.625 | 0.75 | 0.697 | 1.13 | 3.63 | 0.137 | A |
| CB0687 | 0.687 | – | 0.697 | 1.13 | 3.63 | 0.199 | A |
| CB0750 | 0.75 | – | 0.697 | 1.13 | 3.63 | 0.262 | A |
| CB0812 | 0.812 | – | 0.697 | 1.13 | 3.63 | 0.324 | A |
| CB0875 | 0.875 | – | 0.697 | 1.13 | 3.63 | 0.386 | A |
| CB0937 | 0.937 | – | 0.697 | 1.13 | 3.36 | 0.448 | A |
| RCB1000 | 1 | – | 0.741 | 1.375 | 3.88 | 0.212 | C |
| RCB1062 | 1.062 | – | 0.857 | 1.5 | 4 | 0.274 | C |
| RCB1125 | 1.125 | 1 | 0.98 | 1.625 | 4.13 | 0.337 | C |
| RCB1187 | 1.187 | – | 1.103 | 1.75 | 4.25 | 0.399 | C |
| RCB1250 | 1.25 | – | 1.219 | 1.875 | 4.38 | 0.462 | C |
| RCB1312 | 1.312 | – | 1.34 | 2 | 4.5 | 0.524 | C |
| RCB1375 | 1.375 | 1.25 | 1.46 | 2.125 | 5.13 | 0.587 | C |
| RCB1437 | 1.437 | – | 1.581 | 2.25 | 5.25 | 0.649 | D |
| RCB1500 | 1.5 | – | 1.583 | 2.375 | 5.38 | 0.357 | D |
| RCB1562 | 1.562 | – | 1.957 | 2.75 | 5.75 | 0.419 | D |
| RCB1625 | 1.625 | – | 2.076 | 2.875 | 5.88 | 0.482 | D |
| RCB1687 | 1.687 | – | 2.2 | 3 | 6 | 0.544 | D |
| RCB1750 | 1.75 | 1.5 | 2.448 | 3.25 | 6.25 | 0.607 | D |
| RCB1812 | 1.812 | – | 2.815 | 3.625 | 6.63 | 0.669 | D |
| RCB1875 | 1.875 | – | 2.828 | 3.75 | 6.75 | 0.298 | E |
| RCB1937 | 1.937 | – | 3.2 | 4.125 | 7.13 | 0.361 | E |
| RCB2000 | 2 | – | 3.234 | 4.25 | 7.25 | 0.424 | E |
| RCB2062 | 2.062 | – | 3.573 | 4.5 | 7.5 | 0.485 | E |
| RCB2125 | 2.125 | – | 3.822 | 4.75 | 7.75 | 0.548 | E |
| RCB2187 | 2.187 | – | 4.005 | 4.937 | 7.94 | 0.611 | E |
| RCB2250 | 2.25 | – | 4.132 | 5.06 | 8.06 | 0.674 | E |
INDEXABLE COUNTERBORE TOOLS – METRIC
A = cutting diameter · B = shank diameter · L1, L2, L3 = lengths (in.)
| Part No. | A (mm) | Dia. (in.) | B | L1 | L2 | L3 | Pre-Drilled Hole |
|---|---|---|---|---|---|---|---|
| CB1600MM | 16 | 0.63 | 0.75 | 0.697 | 1.13 | 3.63 | 0.142 |
| CB1725MM | 17.25 | 0.679 | – | 0.697 | 1.13 | 3.63 | 0.191 |
| CB1800MM | 18 | 0.709 | – | 0.697 | 1.13 | 3.63 | 0.202 |
| CB1925MM | 19.25 | 0.758 | – | 0.697 | 1.13 | 3.63 | 0.27 |
| CB2000MM | 20 | 0.787 | – | 0.697 | 1.13 | 3.63 | 0.299 |
| CB2200MM | 22 | 0.866 | – | 0.818 | 1.25 | 3.75 | 0.378 |
| CB2225MM | 25 | 0.987 | – | 0.818 | 1.25 | 3.75 | 0.496 |
| CB2800MM | 28 | 1.12 | 1 | 0.947 | 1.5 | 4 | 0.313 |
| CB3000MM | 30 | 1.181 | – | 1.071 | 1.625 | 4.12 | 0.392 |
| CB3150MM | 31.5 | 1.24 | – | 1.194 | 1.75 | 4.25 | 0.451 |
| CB3200MM | 32 | 1.26 | – | 1.317 | 1.875 | 4.37 | 0.471 |
| CB3500MM | 35 | 1.378 | 1.25 | 1.44 | 2 | 5 | 0.589 |
| CB3750MM | 37.5 | 1.476 | – | 1.565 | 2.125 | 5.12 | 0.688 |
| CB3800MM | 38 | 1.496 | – | 1.579 | 2.375 | 5.37 | 0.351 |
| CB4000MM | 40 | 1.575 | – | 1.831 | 2.624 | 5.62 | 0.43 |
| CB4200MM | 42 | 1.654 | – | 2.071 | 2.875 | 5.87 | 0.509 |
| CB4500MM | 45 | 1.772 | 1.5 | 2.317 | 3 | 6.12 | 0.627 |
| CB4750MM | 47.5 | 1.87 | – | 2.722 | 3.75 | 6.75 | 0.292 |
| CB4800MM | 48 | 1.89 | – | 2.912 | 3.937 | 6.94 | 0.312 |
| CB5000MM | 50 | 1.969 | – | 3.088 | 4.125 | 7.12 | 0.391 |
| CB5200MM | 52 | 2.047 | – | 3.274 | 4.312 | 7.31 | 0.47 |
| CB5500MM | 55 | 2.165 | – | 3.548 | 4.5 | 7.5 | 0.588 |
| CB5650MM | 56.5 | 2.224 | – | 3.634 | 4.687 | 7.68 | 0.647 |
| CB6000MM | 60 | 2.362 | – | 3.7 | 4.75 | 7.75 | 0.785 |
INDEXABLE CENTER CUTTING TOOLS
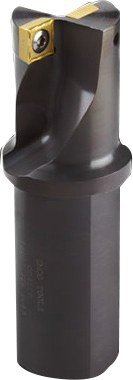
A = cutting diameter · B = shank diameter · L1, L2, L3 = lengths (in.)
| Part No. | A | B | L1 | L2 | L3 | Spare Parts |
|---|---|---|---|---|---|---|
| CC0687 | 0.687 | 0.75 | 0.875 | 1.25 | 3.88 | H |
| CC0750 | 0.75 | – | 0.875 | 1.25 | 3.88 | H |
| CC0812 | 0.812 | – | 0.875 | 1.25 | 3.88 | H |
| CC0875 | 0.875 | – | 0.875 | 1.25 | 3.88 | H |
| CC0937 | 0.937 | – | 0.875 | 1.25 | 3.88 | H |
| CC1000 | 1 | 1 | 1 | 1.5 | 4.25 | F |
| CC1062 | 1.062 | – | 1 | 1.5 | 4.25 | F |
| CC1125 | 1.125 | – | 1 | 1.5 | 4.25 | F |
| CC1187 | 1.187 | 1.25 | 1.12 | 1.75 | 5 | F |
| CC1250 | 1.25 | – | 1.12 | 1.75 | 5 | F |
| CC1312 | 1.312 | – | 1.25 | 2 | 5.25 | G |
| CC1375 | 1.375 | – | 1.25 | 2 | 5.25 | G |
| CC1437 | 1.437 | – | 1.25 | 2 | 5.25 | G |
| CC1500 | 1.5 | 1.5 | 1.25 | 2 | 5.25 | G |
| CC1562 | 1.562 | – | 1.5 | 2.25 | 5.5 | G |
| CC1625 | 1.625 | – | 1.5 | 2.25 | 5.5 | G |
| CC1687 | 1.687 | – | 1.5 | 2.25 | 5.5 | G |
| CC1750 | 1.75 | – | 1.5 | 2.25 | 5.5 | G |
SPARE PARTS
| Spare Part | Insert No. | Screw No. | Wrench |
|---|---|---|---|
| A | CPMT 21.51 | MS-1023 | FT-7 |
| C | TCMT 21.51 | MS-1023 | FT-7 |
| D | TCMT 32.52 | MS-1155 | FT-15 |
| E | TCMT 432 | MS-1158 | FT-15 |
| F | SPMT 32.52 | MS-1168 | FT-15 |
| G | SPMT 432 | CFS-5125 | FT-20 |
| H | SPMT 831 | CSTB 2.2 | FT-7 |
SPEEDS & FEEDS
| Material | SFM | IPT |
|---|---|---|
| Carbon / alloy steels up to 200 BHN | 400 to 600 | 0.003 to 0.005 |
| Hardened steels up to 350 BHN | 300 to 500 | 0.003 to 0.005 |
| Cast iron | 300 to 500 | 0.005 to 0.010 |
| Brass / bronze | 300 to 800 | 0.005 to 0.010 |
| Aluminum | 400 to 1000 | 0.005 to 0.010 |
RPM = (4 × C) ÷ D · Feed IPM = L × T × R
C = surface speed · D = cutter diameter · T = number of effective inserts · R = RPM · L = chip load (IPT)
Counterbore tools have 2 effective inserts; center cutting tools have 1.
These are starting parameters. Listen to the machine and watch for insert wear. If your machine or fixture is not rigid, decrease chip load. If you see insert chipping, increase surface speed and/or decrease chip load.
SPECIALS
Let us take a look at your back spotfacing applications. Our technical staff designs and builds special tools for difficult manufacturing parameters.
ASK ABOUT A SPECIAL TOOL